Choosing the right cable termination methods is one of the most consequential decisions in any custom cable assembly — it determines how reliably a wire joins its connector and how long that joint survives in the field. For B2B buyers specifying harnesses, patch cords, or industrial assemblies, the choice between solder, crimp, and IDC termination changes cost, throughput, rework potential, and failure rate.
What Are Cable Termination Methods?
Cable termination is the process of joining a conductor to a contact, terminal, or connector so current and signal can pass reliably. The three dominant cable termination methods in high-volume manufacturing are soldered joints, crimped contacts, and insulation-displacement (IDC) connections. Each trades speed, tooling cost, and mechanical robustness differently, so the “best” method depends entirely on your application, production volume, and operating environment. Before comparing them, pin down three variables: how many pieces you need, whether the joint will see vibration or moisture, and whether the assembly will ever be reworked.
Solder Termination: When Precision Beats Speed
Solder termination melts a filler alloy around the stripped conductor and the contact, forming a permanent metallurgical bond. It remains the preferred method for low-volume, high-reliability, or mixed-signal assemblies where a technician can visually inspect every joint.
Pros and Cons of Solder Joints
- Strengths: excellent electrical continuity, easy to rework, ideal for prototypes and fine-pitch work.
- Weaknesses: slow, labor-intensive, sensitive to “cold solder” defects, and vulnerable to vibration fatigue in moving applications.
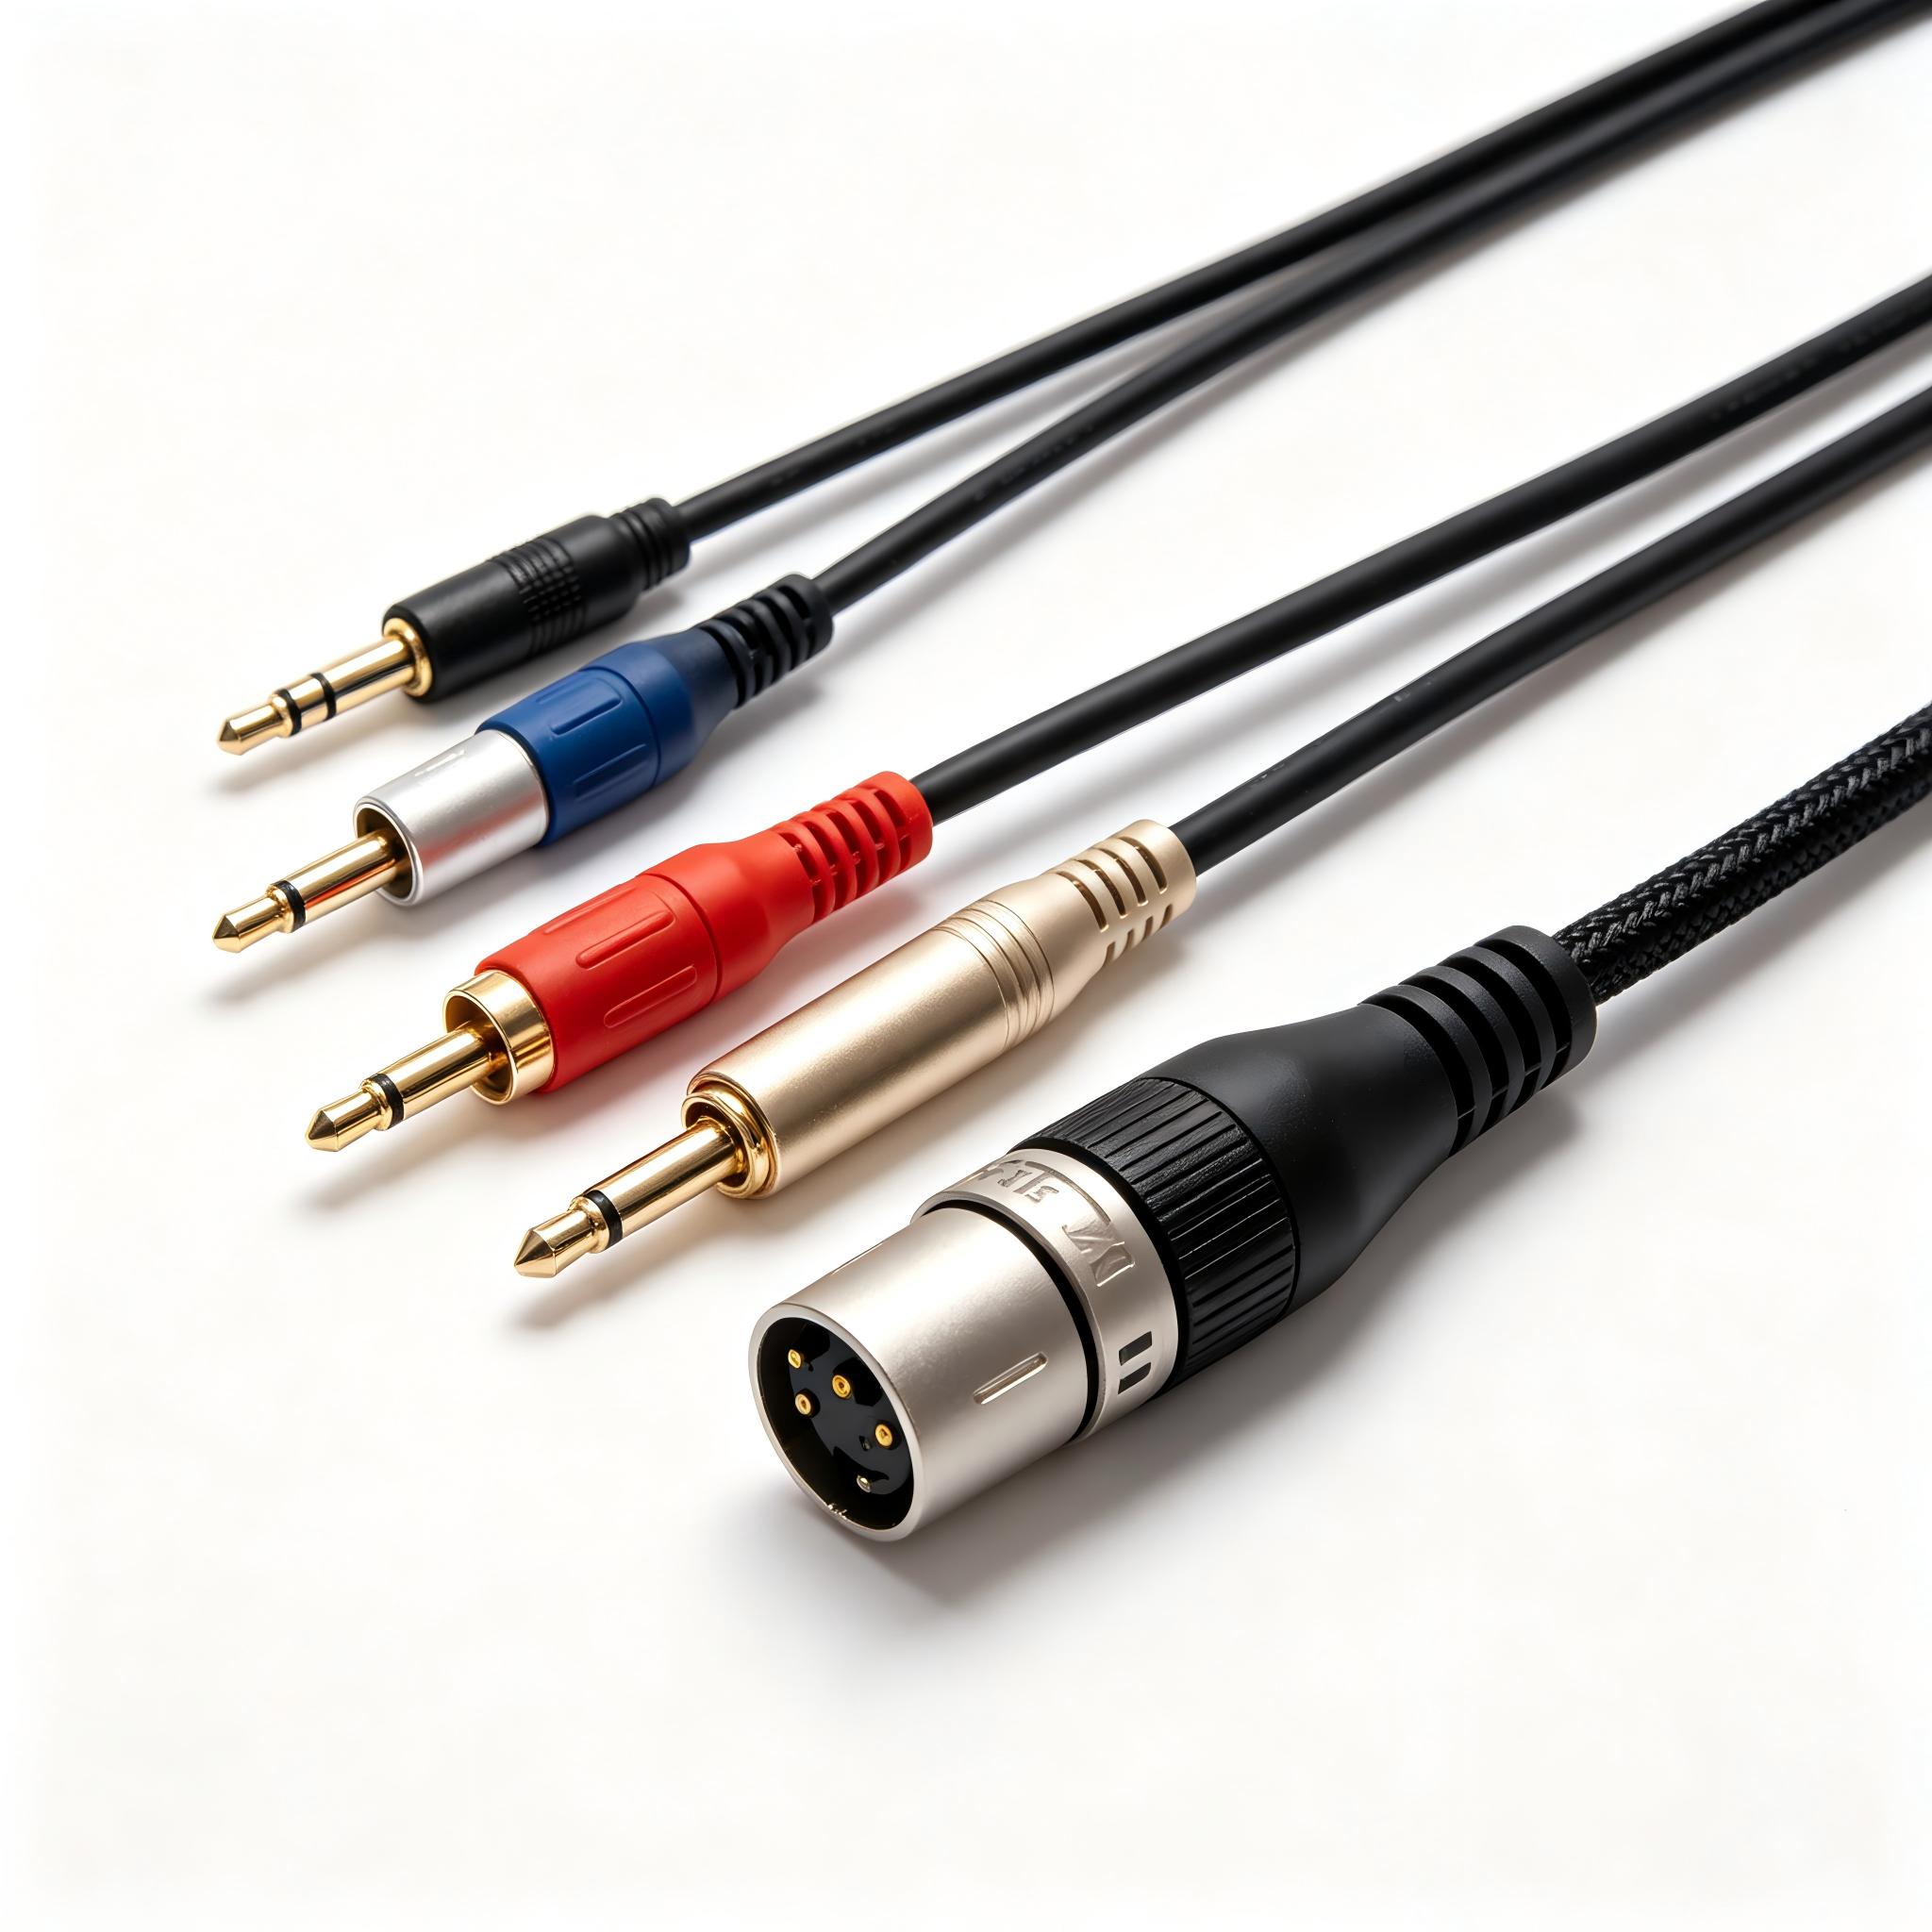
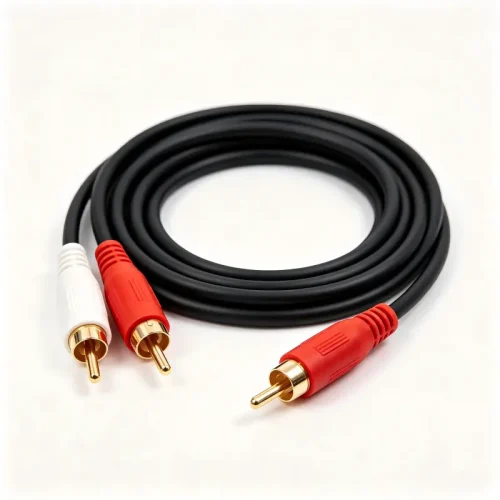
Solder is common on audio cables and custom breakout assemblies where a handful of hand-built joints outperform a crimp tool’s throughput limit.
Crimp Termination: The Industrial Workhorse
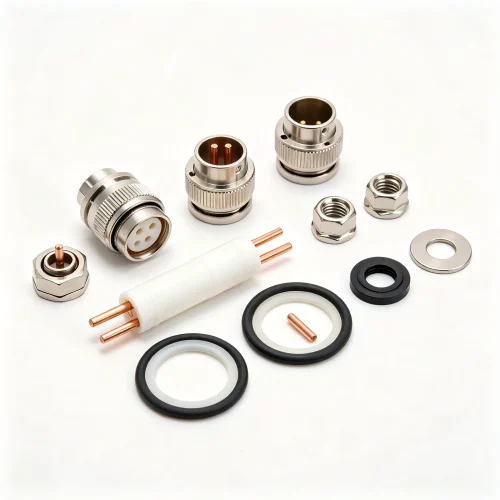
Crimping deforms a metal contact around the conductor using a calibrated die, cold-welding the metals without heat. It is the default for industrial, automotive, and aerospace volumes because a pneumatic or hydraulic press can terminate thousands of contacts per shift with consistent pull strength.
Why Crimp Dominates Production
- Repeatability: proper crimp tooling delivers uniform gas-tight joints.
- Speed: a single press stroke beats minutes of soldering.
- Robustness: resists vibration and thermal cycling far better than solder.
Crimp contacts appear across our serial & industrial communication cables and panel-mount waterproof connectors.
IDC (Insulation-Displacement Connector): Tool-Free Speed
IDC termination slices through a wire’s insulation with a sharp contact blade, displacing it rather than stripping it. The result is a gas-tight connection made in one motion — perfect for ribbon cables, board-to-board headers, and mass-terminated flat cable. Because there is no stripping step, IDC also removes a common source of operator error.
- Strengths: fastest method, no stripping step, low labor cost at scale.
- Weaknesses: limited to specific wire gauges, weaker environmental sealing, harder to rework.
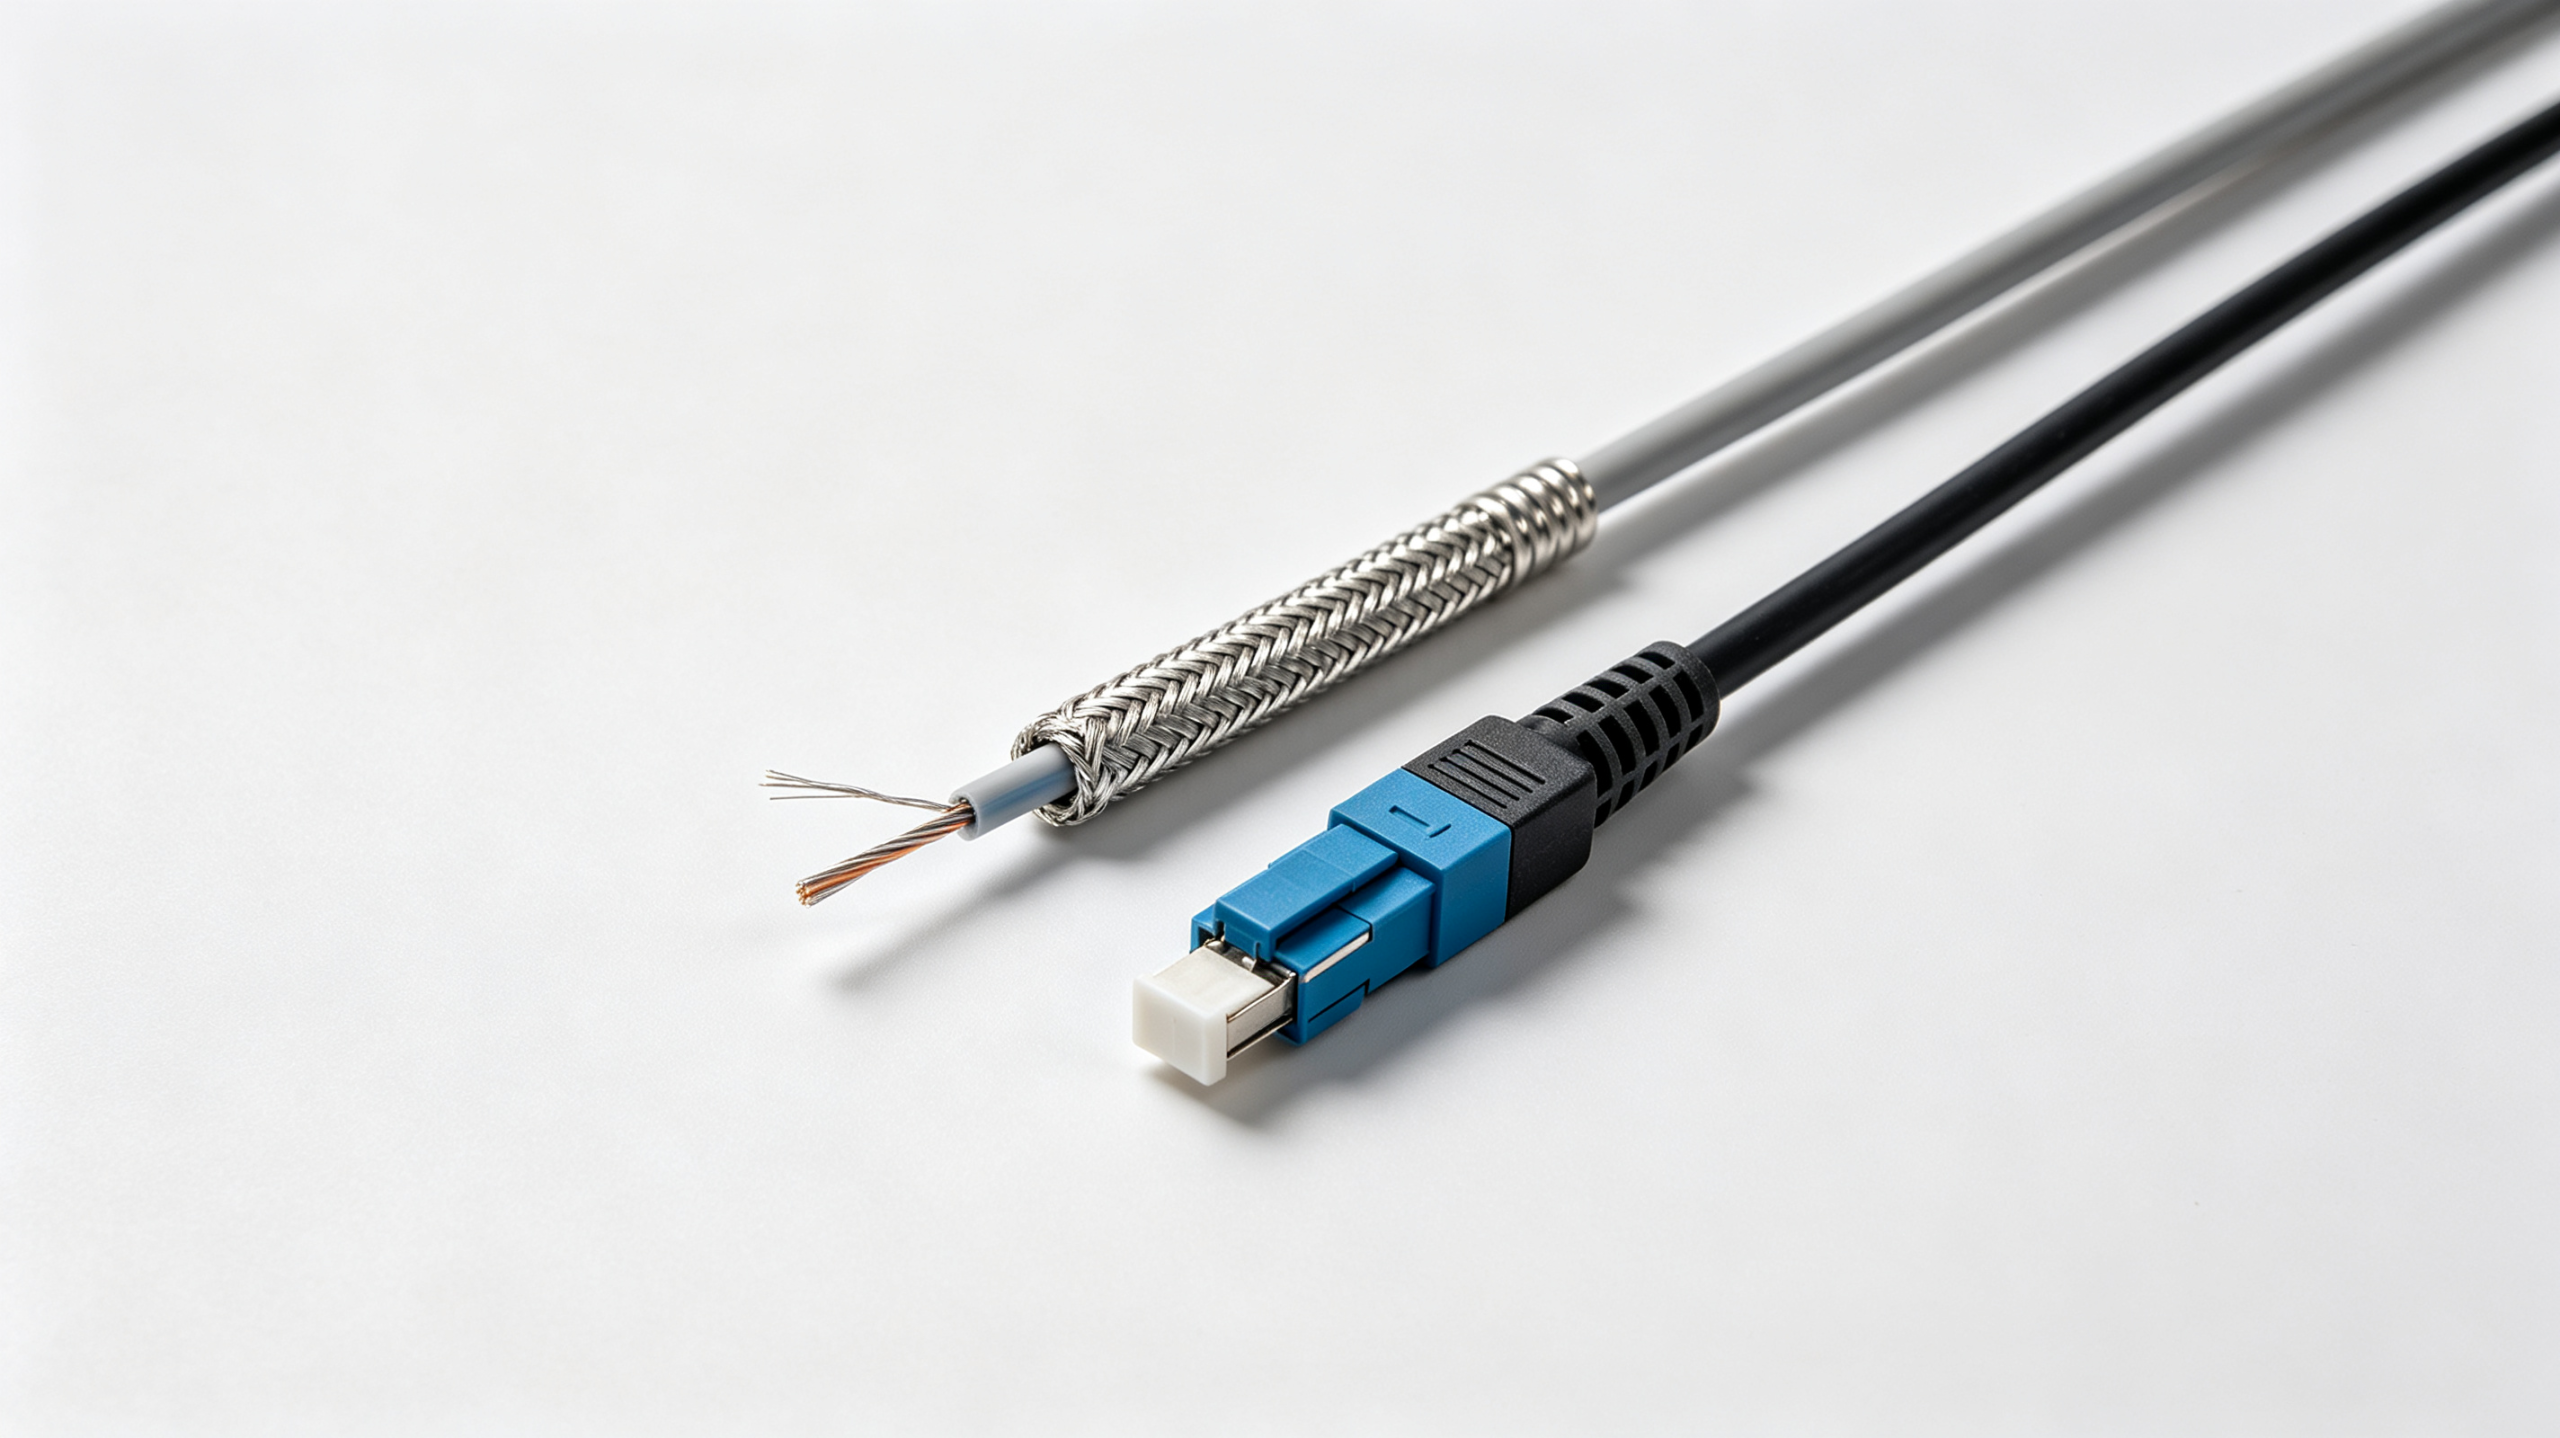
Solder vs Crimp vs IDC: Specification Comparison
The table below summarizes how the three cable termination methods compare on the variables B2B buyers care about most.
| Method | Tooling | Throughput | Rework | Vibration Resistance | Best For |
|---|---|---|---|---|---|
| Solder | Iron + solder | Low | Easy | Fair | Prototypes, fine-pitch, low volume |
| Crimp | Press + die | High | Hard | Excellent | Industrial, automotive, high volume |
| IDC | Hand/rack tool | Very high | Hard | Good | Ribbon, flat, board headers |
How to Specify Cable Termination Methods in Your RFQ
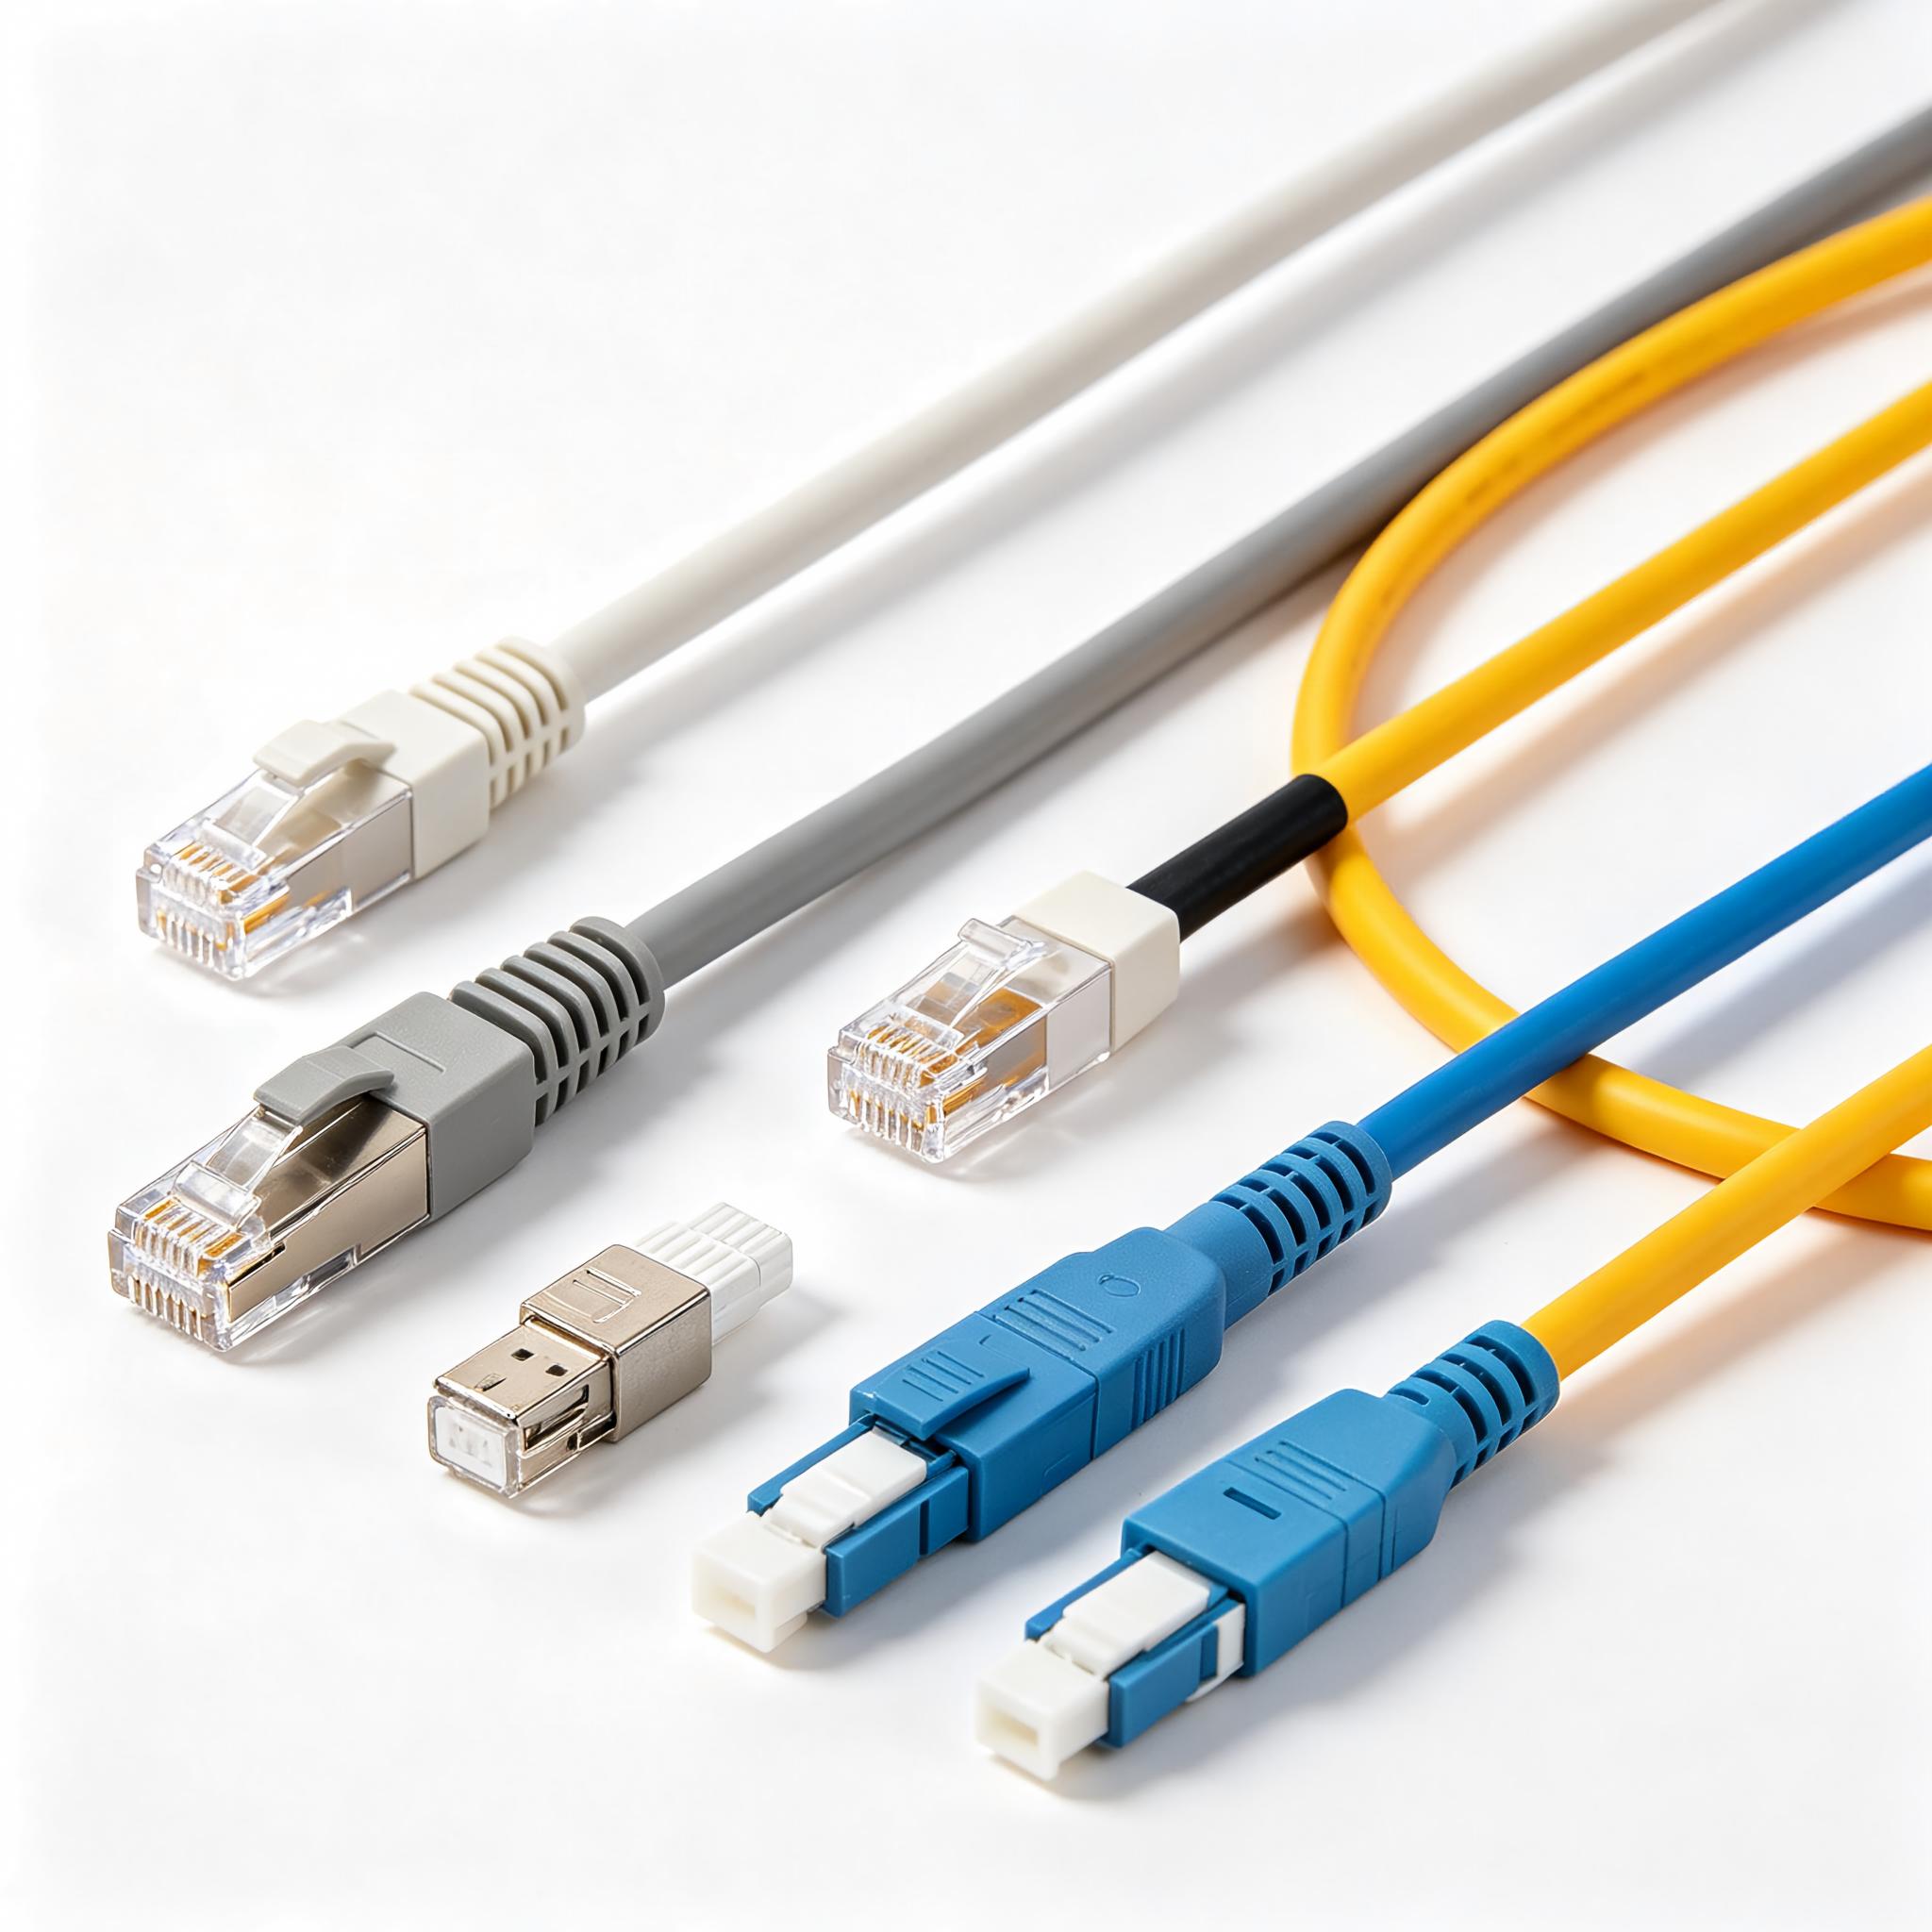
When you send a request for quotation, name the termination explicitly instead of leaving it to the factory. State the contact style (e.g., M12, RJ45, XLR, JST), the target crimp tool/die if known, and the required pull-test or insulation-resistance threshold. Buyers reviewing network & fiber cables should also confirm whether field-terminable or factory-polished connectors are expected.
For a deeper dive into joint mechanics, see the crimp connector reference on Wikipedia.
Common Termination Mistakes B2B Buyers Make
- Assuming “any crimp” is interchangeable — die and contact must be matched.
- Specifying solder for high-vibration harnesses that need crimp robustness.
- Forgetting to request pull-strength or continuity test reports.
- Mixing IDC where environmental sealing is required.
Final Checklist Before You Order
| Check | Why It Matters |
|---|---|
| Method matches volume & environment | Avoids field failures and cost overruns |
| Tooling/die is named | Guarantees repeatable joints |
| Test reports requested | Proof of pull strength & continuity |
| Rework policy agreed | Clarifies scrap handling |
Need help choosing between these adapters & converters and termination styles? Contact our engineering team for a free termination recommendation on your next B2B order.
Termination Cost Model: Build-to-Print vs Build-to-Spec
Beyond the joint itself, the termination choice drives your total landed cost. A build-to-print assembly with named crimp dies shifts tooling cost to the buyer but locks repeatability; a build-to-spec order lets the factory choose tooling and usually lowers unit price at volume. For power cords & power cables and USB cables, standardize on one crimp platform across SKUs so a single die set covers your whole catalog. That consolidation is often the fastest way to cut per-unit termination cost without sacrificing the robustness that crimp joints provide in the field.